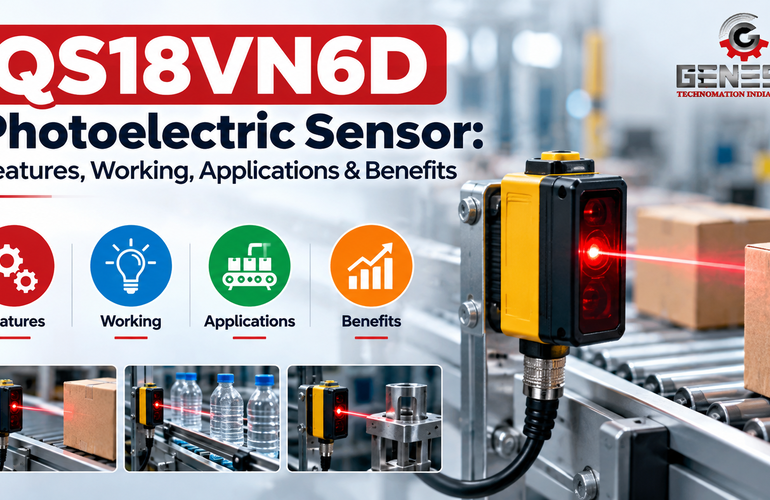
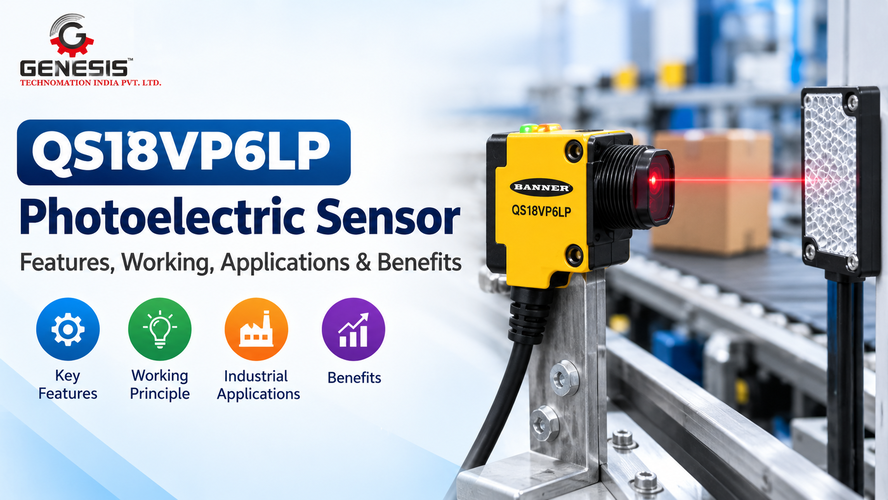
The QS18VP6LP Photoelectric Sensor is a polarized retroreflective sensor manufactured by Banner Engineering for industrial object detection and machine automation. It belongs to the QS18 series and uses a visible red LED, a 10–30 V DC supply and complementary PNP outputs. Its specified maximum sensing range is 3.5 metres, making it a potential option for applications where a sensor must detect objects passing through a defined optical path.
In automated production environments, reliable object detection helps coordinate conveyor movement, packaging operations, product counting and machine sequencing. A sensor that misses a passing product or produces an unexpected switching signal can interrupt a production cycle or cause a controller to respond at the wrong time. Selecting the correct sensor model and configuring it according to the manufacturer’s instructions are therefore essential.
The QS18VP6LP uses a different detection arrangement from diffuse photoelectric sensors. It works with a separate retroreflector, which returns emitted light to the sensor. When an object interrupts the optical path, the sensor changes its output state. This arrangement can be useful when detecting passing objects along conveyors and production lines, provided the target, mounting distance and operating conditions suit the application.
This guide covers the QS18VP6LP Photoelectric Sensor’s specifications, operating principle, detection performance, industrial applications, installation requirements, troubleshooting procedures and purchasing considerations.
QS18VP6LP Photoelectric Sensor: Product Overview
The QS18VP6LP is part of Banner Engineering’s QS18 all-purpose photoelectric sensor series. This exact model is identified as a polarized retroreflective sensor with a 3.5 m sensing range, 10–30 V DC input, complementary PNP outputs and a 2 m cable. Its design also includes an 18 mm mounting nose, a rectangular housing and a visible red sensing beam.
The sensor combines its optical transmitter and receiver in one housing. A separate compatible retroreflector must be positioned opposite the sensor to return the emitted light. The sensor monitors the returned optical signal and detects a target when that signal is interrupted.
This arrangement differs from a diffuse sensor, which detects light reflected directly from the target. With the QS18VP6LP, the optical path is established between the sensor and the reflector. As a result, the installation requires appropriate reflector positioning and clear alignment across the detection area.
The QS18VP6LP is intended for presence detection and related discrete control tasks. It can supply an electrical switching signal to a compatible controller when a target interrupts the beam. The controller can then use that signal in its programmed sequence, such as counting a package or coordinating the next stage of a conveyor process.
Before installation, engineers should distinguish the QS18VP6LP from other QS18-series variants. Models with similar names may use different optical arrangements, output configurations, sensing ranges or connections. The complete model number must match the application requirements.
QS18VP6LP Photoelectric Sensor Features and Specifications
The following table summarizes the technical specifications identified for the QS18VP6LP. Confirm the current manufacturer’s datasheet and exact ordered variant before final design approval.
| Parameter | QS18VP6LP Specification |
| Manufacturer | Banner Engineering |
| Product series | QS18 |
| Model | QS18VP6LP |
| Sensor type | Polarized retroreflective photoelectric sensor |
| Detection principle | Interruption of the returned reflector beam |
| Maximum sensing range | 3.5 m |
| Light source | Visible red LED |
| Wavelength | 630 nm |
| Supply voltage | 10–30 V DC |
| Output configuration | Complementary PNP |
| Switching operation | Light-operate and dark-operate outputs |
| Response time | 0.6 ms |
| Repeatability | 150 µs |
| Power-up delay | 100 ms |
| Connection | 2 m, four-wire cable |
| Housing | Rectangular with M18 mounting nose |
| Housing material | ABS plastic |
| Lens material | Acrylic |
| Protection rating | IP67 |
| NEMA rating | NEMA 4X |
| Operating temperature | −20°C to +70°C |
| Adjustment | Potentiometer |
| Status indication | LEDs |
| Clear-object detection | Not listed as a supported feature |
| Communication interface | Discrete output; IO-Link is not listed as a feature |
What the specifications mean in practice
3.5 m sensing range: The published maximum range provides a starting point for positioning the sensor and reflector. Actual reliability depends on the reflector, alignment, optical conditions and the target’s ability to interrupt the beam. Do not treat the maximum range as a guarantee for every installation.
10–30 V DC supply: The sensor can operate within this specified DC voltage range. The power supply must remain within the permitted limits under normal operating conditions, including any fluctuations present in the machine’s electrical system.
Complementary PNP output: The sensor provides complementary switching outputs. A compatible PLC or controller must support the output arrangement and interpret the relevant signals correctly. Confirm the manufacturer’s wiring diagram before connecting the sensor.
0.6 ms response time: This short response time supports applications involving moving products. However, the complete system’s performance also depends on object spacing, target size, conveyor speed, PLC scan time and the response of downstream equipment.
IP67 protection: This rating indicates protection against dust ingress and temporary immersion under the conditions defined by the applicable standard. It does not automatically make the sensor suitable for every washdown process, aggressive chemical or high-pressure cleaning environment. The model should not be assumed to be washdown-rated.
Complementary operating modes: The manufacturer lists light-operate and dark-operate functionality. These outputs allow the control system to respond to the optical beam’s blocked or unblocked state. The correct signal should be selected according to the machine’s control logic.
Potentiometer adjustment and LED indication: The adjustment control supports sensitivity setting, while the status indicators help technicians observe sensor operation during setup and troubleshooting. Follow the model’s documentation when making adjustments.
Important model-specific limitations
Clear-object detection, IO-Link communication, a dedicated marginal-signal output and timing functions such as hold and delay should not be assumed to be available on the QS18VP6LP. Check the exact product documentation before designing a system that requires these capabilities.
How the QS18VP6LP Photoelectric Sensor Works
The QS18VP6LP uses polarized retroreflective detection. Its transmitter emits visible red light towards a separate retroreflector, and its receiver monitors the light returned from that reflector. A passing object is detected when it interrupts the beam.
The operating sequence is straightforward.
Step 1: Light emission
The QS18VP6LP emits a visible red optical beam towards the retroreflector.
Step 2: Light returns to the receiver
The reflector returns the beam to the sensor while the optical path remains unobstructed.
Step 3: An object interrupts the beam
When a product passes between the sensor and reflector, it blocks the returned light.
Step 4: The output changes state
The sensor’s complementary PNP outputs provide switching signals according to the selected light-operate or dark-operate function.
Step 5: The controller responds
A compatible PLC or machine controller reads the signal and executes its programmed response.
Understanding light-operate and dark-operate functions
For retroreflective detection, light-operate is active when the beam is unblocked, while dark-operate is active when the beam is blocked. The QS18VP6LP has complementary outputs, allowing the relevant switching state to be selected through the appropriate output and control-system configuration.
Consider a packaging conveyor. When a carton passes between the sensor and reflector, the beam is interrupted. The PLC registers the transition and may increment a product counter or initiate a subsequent operation. The precise response depends on the programmed logic, not on the sensor alone.
Correctly configuring the signal matters. If the PLC expects an active signal when the beam is blocked but the wrong output is connected, the machine may interpret the event incorrectly.
Detection Performance of the QS18VP6LP
The published 3.5 m maximum range is useful for planning an installation, but reliable detection depends on the complete optical arrangement. The QS18VP6LP should be evaluated using the actual target, reflector, mounting geometry and operating environment.
Target size and position
A target must interrupt enough of the optical path to produce a dependable switching event. A large carton moving across the beam is generally easier to detect consistently than a very small component passing near the edge of the optical path.
Position the sensor at the point where the target crosses the beam predictably. If the target can move vertically or sideways, test its full range of movement rather than checking only one stationary position.
Surface finish and reflectivity
The QS18VP6LP detects beam interruption rather than relying on the target to reflect light back to the sensor. This is an important distinction when handling dark, glossy or metallic products.
Nevertheless, shiny targets can create optical interference in some retroreflective installations. Polarization helps distinguish the intended reflector return from certain unwanted reflections, but it does not guarantee immunity to every reflective surface or installation geometry. Test highly polished metal, foil packaging and glossy containers under actual operating conditions.
Transparent and translucent objects
Clear-object detection is not listed as a supported feature for the QS18VP6LP. Consequently, applications involving transparent bottles, clear plastic film, glass containers or translucent packaging require particular care.
A transparent target may allow some light to pass through or may not interrupt the beam sufficiently. Do not assume reliable detection simply because the sensor detects opaque cartons on the same line. Conduct representative tests and consider a sensor specifically designed for clear-object detection if the QS18VP6LP cannot meet the requirement.
Distance, alignment and ambient light
The sensor and reflector must remain correctly aligned. Poor alignment, vibration or an obstructed optical path can reduce the reliability of the returned signal.
Ambient light and nearby optical equipment can also affect an installation, depending on the conditions. Position the sensor to minimise interference and verify its operation under normal production lighting.
Machine speed and repeatability
The manufacturer’s listed response time is 0.6 ms, with a repeatability specification of 150 µs. These figures help engineers assess suitability for moving targets, but they do not define a guaranteed maximum conveyor speed or minimum detectable gap.
For high-speed counting, evaluate the entire system. Test the smallest expected product spacing, shortest beam interruption, PLC input filtering and controller scan time. The sensor must have sufficient time to register each event, and the controller must capture the transitions without merging adjacent products into a single count.
Applications of QS18VP6LP Photoelectric Sensor
The QS18VP6LP can be considered for industrial presence-detection tasks where its polarized retroreflective operating principle, range and electrical output meet the application requirements. The following are potential applications, not a claim that the sensor is suitable for every machine listed.
Object detection in automated machinery
Mount the sensor and reflector on opposite sides of a suitable detection point. When a component enters the optical path, the resulting output transition can inform the machine controller that the object has arrived.
This arrangement may support part-presence monitoring, transfer sequencing or confirmation that an item has reached a designated station. Mechanical fixtures should keep the target’s path consistent.
Conveyor systems
On a conveyor, the QS18VP6LP can monitor products passing through a fixed detection zone. Its discrete output can be used by a compatible PLC to trigger counting, diverting, sorting or transfer operations.
For dependable operation, position the beam so that every product crosses it fully. Verify the response with the smallest and most closely spaced products expected during production.
Packaging machines
Packaging lines often require sensors to detect cartons, trays or packages as they move between processing stages. The QS18VP6LP may be suitable when the products reliably interrupt the beam and the mounting arrangement allows the sensor and reflector to remain aligned.
For clear film, transparent containers or products with unusual geometry, validate detection before committing to the design.
Assembly automation
In assembly equipment, the sensor may confirm the arrival of a component at a defined transfer point. A controller can use the signal to permit the next programmed step, provided other required conditions are satisfied.
The sensor does not independently verify correct assembly, orientation or product quality. It detects an optical event. Additional sensing or inspection may be necessary for more complex checks.
Product counting and monitoring
Repeated beam interruptions can support product counting. The 0.6 ms response time provides a useful specification for preliminary design calculations, but the application must be tested at the intended production rate.
If products touch, overlap or leave only a very short gap, individual counts may become unreliable. Validate the system using the actual product dimensions, spacing and conveyor speed.
Carton, bottle and container detection
Opaque cartons and suitable containers that fully interrupt the beam are potential targets. The sensor and reflector should be positioned so that labels, handles or changes in container orientation do not create unexpected gaps in detection.
Transparent bottles require special evaluation because the QS18VP6LP is not listed as a clear-object detection model. Select a different sensing technology if testing demonstrates that the required reliability cannot be achieved.
Material handling and industrial production lines
The QS18VP6LP may also support object-presence monitoring in material-transfer systems, production stations and automated handling equipment. In each case, the engineer must confirm the required sensing distance, mounting space, electrical compatibility, environmental conditions and machine timing.
Benefits of the QS18VP6LP Photoelectric Sensor
The benefits of this model follow from its documented specifications and optical arrangement.
- Longer-distance detection: Its maximum specified range of 3.5 m can support installations where the sensor and reflector need to be separated across a production area.
- Simplified optical arrangement: The transmitter and receiver are contained in one device, so a separate receiver and its wiring are not required.
- Visible optical alignment: The 630 nm red LED makes the sensing beam useful for installation and alignment checks.
- Fast output response: The specified 0.6 ms response time can support suitable moving-product applications after system-level timing tests.
- Controller integration: Complementary PNP outputs provide discrete signals for compatible PLCs and machine controllers.
- Flexible switching behaviour: Light-operate and dark-operate functions allow the detection state to be matched to the intended control logic.
- Environmental protection: The IP67 rating is useful in applications that require the specified level of dust and water-ingress protection, subject to the manufacturer’s installation conditions.
- Sensitivity adjustment: The potentiometer provides an adjustment facility for commissioning and fine-tuning the optical setup.
These benefits do not eliminate the need for correct mounting, maintenance or target testing. A sensor performs reliably when its documented capabilities match the actual process requirements.
QS18VP6LP in Industrial Automation
The QS18VP6LP is a discrete-output sensor rather than a networked measurement device. Its role is to provide an electrical indication of an optical detection event. A PLC or machine controller can use that indication as one input in a larger control sequence.
PLC integration
The sensor’s complementary PNP outputs must be matched to the controller’s input design. PNP outputs generally source positive voltage to a compatible input when active, but the exact wiring and signal interpretation must follow the manufacturer’s diagram.
Before commissioning, check the controller’s input voltage range, common-terminal arrangement, input current requirements and signal filtering. Do not assume that any PLC input can accept a PNP signal.
Conveyors and pneumatic actuators
A conveyor controller can use a detection transition to count an item or initiate a transfer sequence. Where pneumatic actuators are involved, the sensor may supply a condition that allows the controller to command a cylinder or diverter.
The sensor should not directly replace the control logic, interlocks or safety devices required by the machine design. The controller must manage timing, actuator position feedback and fault conditions as appropriate.
Servo and stepper motor systems
Servo-driven and stepper-driven machinery may use the QS18VP6LP to detect products at a fixed point along a transfer route. The controller can use the resulting signal to coordinate a programmed motion or handling sequence.
However, the sensor does not measure shaft position, motor speed or angular displacement. It provides discrete optical detection. Motion accuracy depends on the drive system, control program and other feedback devices.
Industrial control panels
When connecting the sensor to a control panel, engineers should consider cable routing, noise exposure, grounding practices where applicable and the separation of signal wiring from sources of electrical interference. Follow the manufacturer’s wiring and installation instructions, and verify the complete input circuit before enabling automatic operation.
The QS18VP6LP is not a personnel-protection device. It should not be used as a safety sensor for protecting people from hazardous machine movement.
QS18VP6LP Installation and Mounting Considerations
Correct installation has a direct effect on detection reliability. Use the following procedure as a commissioning checklist, while following the manufacturer’s instructions for the exact model.
Confirm the model number
Check that the device is labelled QS18VP6LP. Similar-looking variants may use NPN outputs, different optical modes or alternative cable and connector configurations. A replacement that fits mechanically may still be electrically or optically unsuitable.
Position the sensor and reflector
Mount the sensor and compatible retroreflector opposite one another so the beam travels through the intended detection zone. Use the specified sensing range as the maximum design reference, and allow for practical installation tolerances.
The reflector must be suitable for the sensor’s polarized retroreflective mode. Confirm reflector compatibility rather than selecting an arbitrary reflective surface.
Align the optical path
Adjust the mounting positions until the sensor receives a stable return from the reflector. Test the installation by passing representative products through the beam. Include variations in size, orientation and speed.
Secure the mounting hardware to prevent vibration from shifting the optical alignment. Recheck the setup after nearby mechanical work or equipment relocation.
Verify the power supply and output circuit
The specified supply is 10–30 V DC. Confirm that the voltage at the sensor terminals remains within this range during operation.
Connect the complementary PNP outputs according to the official wiring diagram. The standard QS18VP6LP uses a 2 m four-wire cable. Do not infer wire assignments from another model or rely solely on generic colour conventions without checking the manufacturer’s documentation.
Check the operating environment
The specified operating temperature is −20°C to +70°C. Confirm that the sensor location stays within this range and that the installation is appropriate for the site’s dust, moisture and cleaning conditions.
Although the product has an IP67 rating, it should not automatically be treated as suitable for high-pressure washdown. Where frequent cleaning or chemical exposure is expected, verify suitability before installation.
Test the complete machine sequence
After mounting and wiring, verify the output state with the optical path both clear and blocked. Confirm that the PLC interprets each state correctly.
Then test the sensor during actual production. Check normal and maximum operating speeds, product spacing and any expected variation in target position. Do not approve the installation based only on a stationary bench test.
Factors Affecting QS18VP6LP Detection
Several conditions can cause inconsistent detection even when the sensor is electrically functional.
| Potential issue | Why it matters | Recommended action |
| Incorrect alignment | The reflector’s return may not reach the receiver consistently. | Realign the sensor and reflector and secure their mounts. |
| Unsuitable reflector | An incompatible reflector may not return the optical signal as expected. | Verify reflector suitability for polarized retroreflective operation. |
| Incorrect sensing distance | Excessive separation or poor alignment can reduce the available optical signal. | Check the installation against the specified range and manufacturer’s guidance. |
| Shiny target surfaces | Unwanted reflections may interfere with some optical arrangements. | Test the target and adjust the mounting geometry where possible. |
| Transparent objects | The beam may not be interrupted sufficiently for reliable detection. | Validate the actual target or consider a dedicated clear-object sensor. |
| Dust or contamination | Deposits on the optical surfaces or reflector can reduce returned light. | Inspect and clean the optical surfaces using approved methods. |
| Mechanical vibration | Movement can disturb sensor-to-reflector alignment. | Improve mounting rigidity and inspect the supporting structure. |
| Excessive product speed | The interruption may be too brief for the complete control system to register reliably. | Check response time, PLC input filtering and controller scan time. |
| Incorrect electrical connections | The output may not reach the intended PLC input correctly. | Verify the official wiring diagram, supply voltage and PNP compatibility. |
| Electrical interference | Noise may disturb the control signal in some installations. | Inspect cable routing and apply appropriate industrial wiring practices. |
| Incorrect output interpretation | The PLC may respond to the opposite switching state from the one intended. | Verify the selected light-operate or dark-operate signal and PLC logic. |
Treat these as possible causes, not evidence of a defect in the QS18VP6LP. Troubleshooting should begin by observing the actual sensor state and comparing it with the controller input.
QS18VP6LP Maintenance and Troubleshooting
Routine inspection helps identify alignment changes, contamination and electrical faults before they lead to recurring production interruptions.
| Problem | Possible cause | Recommended action |
| Target is not detected | Incorrect alignment, unsuitable reflector or target, or excessive distance | Check the optical path, reflector and mounting distance. |
| Intermittent detection | Vibration, contamination or loose electrical connections | Inspect mounting hardware, optical surfaces and connections. |
| False triggering | Optical interference or incorrect setup | Check alignment, ambient conditions and target movement. |
| PLC does not register the output | Wiring fault or electrical incompatibility | Verify the documented PNP output arrangement, supply voltage and PLC input. |
| Detection fails at higher speeds | Response-time or input-filtering limitations | Review the sensor response specification alongside controller timing and product spacing. |
| Detection varies between products | Different target dimensions, positions or surface properties | Test representative products and standardise the detection path where possible. |
| Indicator activates but machine does not respond | PLC logic, input configuration or downstream interlock issue | Check the physical input status and programmed sequence. |
| Detection becomes less reliable over time | Contamination, mounting movement or environmental changes | Clean the optical surfaces appropriately and inspect the mounting and surroundings. |
Recommended maintenance procedure
First, place the machine in a safe maintenance state and follow the site’s lockout procedures where required. Never reach into moving equipment to test a sensor.
Inspect the housing, cable and mounting hardware for damage. Check the reflector and sensor’s optical surfaces for contamination, and clean them using the manufacturer’s approved procedure.
Next, test detection with the beam clear and blocked. Observe the sensor indicators and compare the physical output with the PLC input status. If the sensor output changes but the controller does not register the signal, investigate the wiring, input configuration and program logic before replacing the sensor.
If the problem persists, consult the official QS18VP6LP datasheet and product manual. Avoid opening the housing or attempting internal repairs. Follow the manufacturer’s repair and replacement recommendations.
Why Consider the QS18VP6LP for Industrial Applications?
The QS18VP6LP may be worth evaluating when a machine requires polarized retroreflective detection, a maximum sensing distance of 3.5 m, a 10–30 V DC supply and complementary PNP outputs.
For original equipment manufacturers, its documented specifications provide a basis for designing the optical path, mounting arrangement and controller interface. Automation integrators can assess whether the output and response time suit a particular production sequence. Maintenance teams can use the visible beam, status indicators and adjustment facility during commissioning and fault diagnosis.
The model is not automatically suitable for every application. A machine requiring reliable clear-bottle detection, a different output type, a networked communication interface or washdown-specific construction may require another sensor.
The right selection decision comes from comparing the exact model’s specifications with the application’s requirements, then validating performance using the actual target and operating environment.
Where to Buy QS18VP6LP Photoelectric Sensor in India
Industrial buyers should confirm the exact model number, technical specifications and supply availability before ordering a replacement or selecting a sensor for new equipment.
Genesis Technomation India Pvt. Ltd. is a purchasing enquiry option for industrial automation products and sensor requirements in India. Buyers can visit its product page to enquire about the QS18VP6LP Photoelectric Sensor, technical documentation, pricing and suitability for their application.
Looking to buy a QS18VP6LP Photoelectric Sensor?
Visit Genesis Technomation’s photoelectric sensor page to enquire about photoelectric sensors and related industrial automation requirements.
Before placing an order, confirm the exact Banner Engineering model, cable configuration, output type and current availability with the supplier.
Industrial buyers, OEMs, packaging-machine manufacturers, automation integrators and maintenance teams should provide their application details when enquiring. Include the required sensing distance, target material, operating speed, controller type and installation environment.
Do not assume that a product is in stock, that a specific price applies or that a supplier has authorised-distributor status without confirmation. Request the current quotation and relevant product documentation before purchasing.
QS18VP6LP Buying Considerations
Use this checklist when evaluating the QS18VP6LP Photoelectric Sensor for an industrial application.
- Exact model: Verify QS18VP6LP and check that the suffix matches the required cable and output configuration.
- Detection principle: Confirm that polarized retroreflective sensing is suitable for the target and mounting arrangement.
- Sensing range: Determine whether the specified maximum distance of 3.5 m meets the actual installation requirement.
- Target characteristics: Consider product dimensions, shape, transparency, reflectivity and orientation.
- Operating speed: Check whether the response time and PLC input timing support the required detection rate.
- Electrical compatibility: Verify the 10–30 V DC supply and complementary PNP outputs against the controller specifications.
- Cable requirements: Confirm that the standard 2 m cable is long enough for the installation and that the wiring arrangement matches the control panel.
- Mounting dimensions: Review the manufacturer’s mechanical drawing and allow space for the sensor, reflector and mounting hardware.
- Environmental conditions: Check temperature, dust, moisture, vibration and cleaning requirements against the documented ratings.
- Protection requirements: Confirm whether IP67 and NEMA 4X are appropriate for the installation. Do not assume the sensor is suitable for high-pressure washdown.
- Documentation: Obtain the official datasheet, wiring diagram and installation manual.
- Supplier support: Confirm pricing, availability, delivery arrangements and assistance with technical selection.
Completing these checks before ordering helps prevent avoidable compatibility problems and reduces the risk of choosing a sensor that cannot reliably detect the intended target.
FAQs About QS18VP6LP Photoelectric Sensor
What is the QS18VP6LP Photoelectric Sensor?
The QS18VP6LP is a Banner Engineering QS18-series polarized retroreflective photoelectric sensor. It uses a visible red LED, has a maximum specified sensing range of 3.5 m and provides complementary PNP outputs for compatible industrial control systems.
How does the QS18VP6LP sensor work?
The sensor emits a red optical beam towards a separate retroreflector. When an object interrupts the returned beam, the sensor changes its output state. A compatible PLC can use that signal to trigger a programmed machine operation.
What are the main features of QS18VP6LP?
Its documented features include polarized retroreflective sensing, a 3.5 m maximum range, a 10–30 V DC supply, complementary PNP outputs, a 0.6 ms response time, a 2 m cable, IP67 protection, LED indicators and potentiometer adjustment.
What are the specifications of QS18VP6LP?
The model has a 630 nm visible red LED, a 10–30 V DC operating supply, complementary PNP outputs, a 0.6 ms response time and a maximum sensing distance of 3.5 m. Its specified operating temperature is −20°C to +70°C. Consult the manufacturer’s official documentation for the complete specifications and wiring details.
What are the industrial applications of QS18VP6LP?
Potential applications include conveyor product detection, carton counting, packaging equipment, component-presence monitoring and material handling. Suitability depends on whether the target reliably interrupts the beam and whether the electrical and timing requirements match the machine.
What factors affect QS18VP6LP detection performance?
Alignment, reflector compatibility, sensing distance, target geometry, transparent materials, contamination, vibration and operating speed can influence detection reliability. The best way to evaluate performance is to test representative targets under actual production conditions.
How should the QS18VP6LP be installed?
Mount the sensor opposite a compatible retroreflector, align the optical path and secure the mounting hardware. Verify the supply voltage, complementary PNP output wiring and PLC input compatibility using the manufacturer’s diagram. Test the installation before enabling automatic operation.
What should I check if the QS18VP6LP does not detect an object?
Inspect the alignment, reflector, sensing distance and optical surfaces first. Then check the sensor indicators, supply voltage, output wiring and PLC input status. If the problem continues, consult the official manual and use manufacturer-approved troubleshooting procedures.
Can the QS18VP6LP be connected to a PLC?
Yes, it can be connected to a PLC with a compatible DC input circuit that supports its complementary PNP output arrangement. Verify the wiring diagram, input voltage and switching logic before connecting the sensor. The correct interface depends on the PLC model and control-panel design.
Where can I enquire about the QS18VP6LP price in India?
You can enquire through Genesis Technomation India Pvt. Ltd.’s photoelectric sensor product page. Request a current quotation and confirm availability, the exact model number, technical documentation and suitability for your application.
Conclusion
The QS18VP6LP Photoelectric Sensor is a polarized retroreflective sensor from Banner Engineering’s QS18 series. Its documented 3.5 m maximum sensing range, visible red LED, complementary PNP outputs, 0.6 ms response time and 10–30 V DC supply make it a candidate for suitable object-detection tasks in industrial automation.
Its performance depends on more than the published range. Correct reflector selection, optical alignment, target characteristics, electrical compatibility and controller timing all influence whether the sensor can meet a production requirement. Applications involving transparent products or demanding washdown conditions require particular scrutiny because the model is not listed as a clear-object detection or washdown-rated sensor.
Before installation or replacement, verify the complete model number and review the manufacturer’s datasheet and wiring instructions. Test the sensor with representative products under actual operating conditions, and ensure that the connected control system interprets the output correctly.
For purchasing enquiries and assistance with industrial photoelectric sensor requirements, visit Genesis Technomation India Pvt. Ltd. and confirm the QS18VP6LP model’s availability and technical suitability before ordering.
Related Posts